Dearborn, Michigan. A Summer Evening. 1896.
He built it in a coal shed behind his rented house on Bagley Avenue.
His wife Clara held a lantern while Henry Ford finished tightening the last bolt on a four-wheeled contraption powered by a two-cylinder gasoline engine. He called it the Quadricycle. It weighed less than 500 pounds. It had no reverse gear. It barely fit through the shed door, which he had to remove with an axe to get the thing outside.
He climbed on, struck the engine, and drove into the dark Detroit street at four in the morning on June 4, 1896.
No suppliers. No logistics network. No forecasting model. Just one man, one machine, and a lantern held by a woman who believed in him.
It would never be that simple again.
Four Dates That Changed Manufacturing Forever
The Quadricycle
Ford built his first self-propelled vehicle in a coal shed on Bagley Avenue, Detroit. He drove it into the street at 4am on June 4, 1896. It was the last time his supply chain would be a single man in a single shed.
Ford Motor Company Founded
On June 16, 1903, Ford and twelve investors pooled $28,000 and incorporated the Ford Motor Company on Mack Avenue, Detroit. They sold their first car, a Model A, on July 23. By October 1, they had turned a profit of $37,000. Ford produced 1,708 cars that first year. The investors breathed out. Ford breathed in, and started planning something larger.
The Model T
On October 1, 1908, the first Model T rolled out of the Piquette Avenue plant. Ford had promised a car for "the great multitude." The price was $825. Within a year, it was outselling every other car on the market. Demand did not rise. It erupted. By 1910 Ford was producing over 19,000 Model Ts annually. By 1912, that number had crossed 78,000. The supply chain was beginning to buckle under the weight of his own success.
The Moving Assembly Line
Ford's engineers, inspired partly by the overhead conveyor systems of Chicago meatpacking plants, began experimenting with a moving chassis assembly line at Highland Park in August 1913. The results were staggering: the time required to assemble a single Model T chassis dropped from 12.5 man-hours to just 93 minutes. The world hailed it as a miracle of engineering. What the journalists did not see was the supply chain crisis it had just created.
1903 and the First Supply Chain Fracture
When Ford Motor Company was incorporated on June 16, 1903, in a modest Detroit shop with $28,000 in capital, Henry Ford believed he understood manufacturing. He had worked at Edison's plant. He had tinkered obsessively. He knew machines.
What he did not know was that supply chains are harder to control than machines.
The early Model A and Model C production required coordinated sourcing from dozens of suppliers across Michigan, Ohio, and Pennsylvania. Engines came from one vendor. Transmissions from another. Axles from a third. Body parts from a fourth. And none of these suppliers talked to each other.
Ford's early purchasing agents, scrambling to keep the lines fed, developed what historians would later call "hand-to-mouth inventory" management: ordering only what was needed, almost when it was needed, trusting suppliers to deliver and praying they would. It worked when the volumes were small. At 1,708 cars a year, the chaos was manageable.
What Ford did not know yet was that he was building a machine that would soon demand ten times that volume. And the supply chain behind it was already cracking.
Ford experienced what modern supply chain professionals would recognise immediately: demand-supply misalignment, visibility collapse, and the bullwhip effect, decades before it would be formally named.
The assembly line facilitated an exceptional degree of internal control, but it also called for an unprecedented degree of external coordination. From the beginning, mass production was networked production.Damon Yarnell, University of Pennsylvania, on the Ford supply network, 2009. Verified peer-reviewed academic research.
Imagine if, in 1903, Ford had possessed access to what we now call S&OP (Sales and Operations Planning) and demand-driven supply chain orchestration. Real-time visibility into supplier capacity and inventory. Integrated demand forecasting that linked actual dealer orders to production schedules. Automated variance alerts when suppliers deviated from commitments. Collaborative planning dashboards showing every node in the supply chain network.
Instead, Ford solved it the only way he knew: vertical integration. He bought the suppliers. He owned the mines, the mills, the forests. He controlled the entire chain from iron ore to finished car.
It worked, but at a cost. Flexibility vanished. Responsiveness died. The model would eventually crumble when markets demanded variety.
1908 and the Invisible Crisis Behind the Model T Miracle
On October 1, 1908, the Model T rolled off the assembly line at Piquette Avenue in Detroit. The world changed that day. Affordability met engineering. A car for "the great multitude" was no longer a dream.
What the public did not see was the supply chain near-collapse that almost prevented it.
Demand for the Model T exploded beyond every projection. Ford had estimated production of around 2,000 vehicles in the first year. By 1910, dealers were ordering 19,000. By 1912, 78,000.
The supply chain could not breathe.
The fundamental problem was one that supply chain professionals would recognise in an instant: demand had scaled faster than supply visibility.
Ford had no forecasting system beyond dealer telegrams and handwritten letters. By the time he understood the true shape of demand, he was already three months behind it. Suppliers received orders with little notice and even less context. They could not plan their own capacity because they had no window into Ford's actual requirements. They guessed. Ford guessed. And the gap between the guesses cost everyone money.
Charles Sorensen, Ford's chief production engineer and one of the architects of the assembly line, later wrote in his memoir "My Forty Years with Ford":
"We were constantly fighting fires. A shortage here, an overage there. The supply problem was always present."
Charles Sorensen, Chief Production Engineer, Ford Motor Company. Verified published memoir.That was not the colourful polemic of a man exaggerating for posterity. That was the sober recollection of an engineer who spent years trying to synchronise a supply chain that had no language for synchronisation.
Ford's operations team, instead of chasing supplier telegrams, could have sat down each morning with an AI supply chain expert trained not on generic business advice but on the specific frameworks of demand-driven manufacturing. Here is what each mode would have changed:
The SCMDOJO Supply Chain Management Track covers precisely the frameworks Ford was missing in 1908: S&OP fundamentals, demand forecasting methods, supplier relationship management. Had Ford's operations team studied these disciplines formally rather than discovering them painfully through experience, the supply disruptions of 1908 to 1913 might have looked very different.
Instead, Ford did what brilliant, impatient industrialists do when the system fails them: he decided to own the system.
1913 and the Supply Chain the Assembly Line Almost Destroyed
December 1913. Highland Park Plant. The moving assembly line had debuted and it changed manufacturing forever.
Ford had reduced the time to assemble a chassis from 12.5 hours to 93 minutes. Labor costs dropped. Production capacity doubled. The Model T's price fell and dealers lined up around the block.
The public celebrated the assembly line as a triumph of engineering genius.
Behind the scenes, it created a supply chain crisis that nearly destroyed the company.
The moving assembly line was merciless. It demanded materials at precise intervals. A 2-minute cycle time meant that every component had to arrive at exactly the right moment: not 10 minutes early (inventory piles up), not 10 minutes late (the line stops, and thousands of workers stand idle).
The Highland Park plant suffered a number of work stoppages because of supplier failures. These were not small inconveniences. Each stoppage cost Ford wages for every idle worker on the floor.
Damon Yarnell's peer-reviewed research on Ford's supply network, published through the University of Pennsylvania, established a finding that remains startling even today:
"Through 1916, Ford relied on outside suppliers for about half of the 5,000 parts in each Model T. Five thousand parts. Dozens of suppliers. And none of them fully understood the synchronisation requirements the moving line had just imposed on the entire network."
Damon Yarnell, "Hand-to-Mouth Inventory and the Model T: Outside Supply at the Ford Motor Company, 1908-1927." Verified peer-reviewed academic research.In January 1914, Ford made one of his most famous decisions: he raised his workers' minimum daily wage to $5.00, more than double the industry standard. It was a supply-side insight applied to labour. Ford understood that if he controlled the quality and stability of his workforce, the factory would run better.
He never applied the same insight to his supply chain. He never asked: what would happen if we shared our production schedules with suppliers months in advance, so they could plan their own capacity? What if, instead of treating them as interchangeable vendors, we treated them as partners whose stability was as important as our workers' stability?
These are the questions that SCMDOJO's Supplier Relationship Management course is built on. They are the questions Ford never thought to ask in 1913, because no framework existed to help him ask them.
Instead, he found another answer entirely.
This section is entirely fictional. The supply chain principles are entirely real.
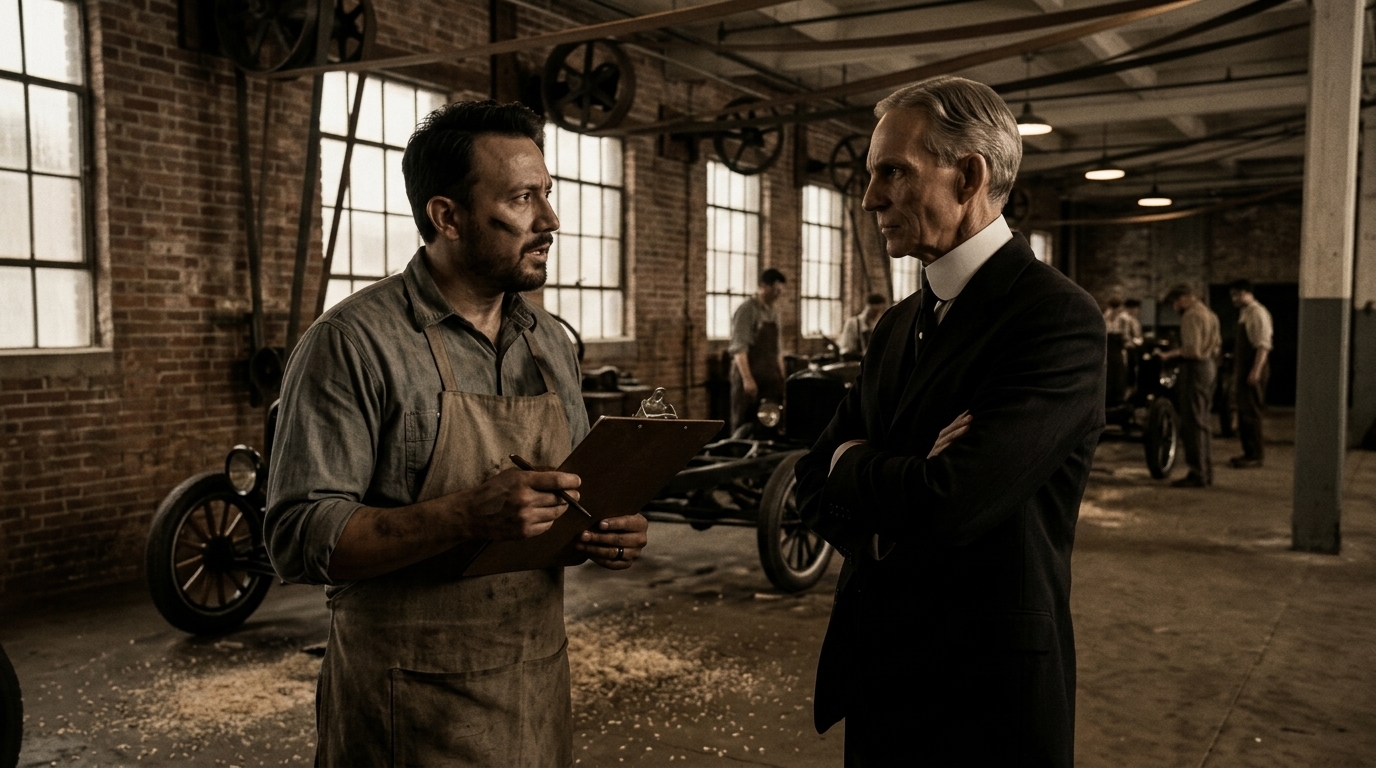
Late January 1914. 11pm. The Highland Park plant running a night shift, the floor lit by electric lights and loud with the mechanical percussion of the assembly line.
Ford stood at the line's edge watching a chassis move past him on the chain. Perfect synchronisation. Every worker knowing their task. Every motion stripped of waste. He had built something extraordinary here.
And yet. Three stoppages this month. Axle shortage from the Toledo supplier. Wheel delivery late from Budd Manufacturing. Carburetor parts arriving in the wrong sequence and piling up at the wrong station.
He heard footsteps behind him.
The figure who approached him was carrying something that glowed faintly blue in the industrial dark.
The River Rouge and the Lesson It Teaches
Ford began acquiring land along the Rouge River in 1915. Construction started in 1917. By the late 1920s, the River Rouge complex was processing its own iron ore, making its own steel, generating its own power, and assembling finished cars within a single site. Ford's quest for vertical integration hinged on the idea of continuous flow: "from earth to assembly," without pause for warehousing or storage.
It worked, completely and magnificently, for exactly as long as the market wanted a single product in a single colour.
When General Motors, led by Alfred Sloan, introduced "a car for every purse and purpose" in the mid-1920s, the River Rouge became exactly what the midnight visitor had predicted: a monument to inflexibility. In 1927, Ford was forced to shut the entire complex down for almost a year to retool for the Model A. His market share, which had once exceeded 60 percent of the American automobile market, had collapsed.
He had solved the supply chain coordination problem through ownership. It was brilliant. It was expensive. It was, ultimately, the wrong answer.
The right answer was always visibility.
The way to make automobiles is to make one automobile like another automobile, to make them all alike, to make them come through the factory just alike, one after the other.Henry Ford, "Today and Tomorrow", 1926. What Ford did not have was the intelligence to see why that standardisation was necessary, or the tools to achieve it without owning everything.
Ford understood flow. He understood waste. He understood that every step in a process that did not add value was a step to be eliminated. He was, in the truest sense, the father of operational efficiency.
What he lacked was a system that could make his supply chain as legible as his factory floor. A system that could show him demand signals forming months before they arrived at his gate. A system that could score his supply chain maturity, rank his risk exposures, synchronise his supplier relationships, and generate the standard operating procedures his growing organisation needed.
Ford had genius. What he lacked was sight. And sight, it turns out, is the one thing you cannot build in a factory.
The Ghosts in the Machine
On a cold morning in January 1914, Henry Ford stood in the Highland Park facility, watching the assembly line run at full speed. A completed chassis rolled off every 12 minutes. Workers moved in synchronised rhythm. The whole factory hummed like a perfectly calibrated engine.
But somewhere in the supply network, in a foundry in Cleveland, on a rail line outside Pittsburgh, in the leather workshops of Newark, materials were moving imperfectly, arriving late, stacking up, causing invisible delays.
Ford did not know this. The visibility did not exist.
Had he possessed a dashboard showing the true state of his entire supply chain, the bottlenecks, the risks, the opportunities for coordination, he might have made a different decision about the River Rouge.
Instead, he built it.
And for 13 years, it was the most impressive manufacturing facility on Earth.
Then markets changed. Competitors adapted. And the very system that made Ford dominant made him inflexible.
The River Rouge still stands today, a monument to brilliant engineering and supply chain blindness.
Perhaps the real lesson is this: supply chain excellence is not about control. It is about visibility. And visibility requires humility, the humility to acknowledge that you cannot see everything, and therefore need systems that help you see it.
Ford had genius. What he lacked was sight.
What Ford Would Have Had Access To
The tools, frameworks, and knowledge base that could have changed every decision Ford made between 1903 and 1927 exist today. Supply chain professionals use them every day.
Ford had genius. You have sight.
The visibility Ford spent $200 million trying to buy through vertical integration is available to any supply chain leader today. Start with a free account on SCM SENSEI AI.